The future of manufacturing is being built by automation. That future is already here — it’s called Industry 4.0 — and it’s driven by robotics, PLCs, and CNC technology.

If you’re already in the machining trade or want to break into it, transitioning from CNC Operator or CNC Machinist to CNC Programmer is one of the smartest moves you can make. And the best place to start? School.

Why CNC Programming Is the Next Step

A CNC Programmer is the person behind the code that tells machines how to move, cut, and shape parts. The job requires a solid understanding of materials, machine operations, tooling, and software. It’s high-skill work, and demand is growing across every sector of U.S. manufacturing.

So if you’re committed to becoming a CNC Programmer, start by enrolling in a technical college or trade school that offers a certificate, diploma, or associate degree in CNC Programming.

Here’s what to consider as you explore your options.

How to Choose the Right CNC Program

1. Look for NIMS Accreditation

The National Institute for Metalworking Skills (NIMS) is the gold standard in CNC training. Schools with NIMS-accredited programs follow a curriculum that aligns with current industry needs — which means you’ll graduate ready to work.

NIMS also offers CNC Programmer Certification, which can boost your résumé and credibility on day one.

2. Check for Hands-On Training and Software Access

Quality CNC programs give you access to:

  • Modern machine tools
  • Industry-standard software
  • Real-world shop environments

If your school teaches Mastercam, you’re in good shape. It’s one of the most widely used CNC programming platforms in the industry, and it’s what many employers expect their programmers to know.

3. Weigh the Length of the Program

Your time matters. Here’s a breakdown of typical options:

  • Certificate – fastest path, focused curriculum
  • Diploma – adds more coursework and training hours
  • Associate Degree – two-year commitment, broader education

Choose the one that fits your schedule, goals, and learning style.

4. Understand the Cost and Value

Cost varies widely by program and location. Make sure you’re getting real value in return — up-to-date equipment, experienced instructors, and job placement support.

And don’t forget to ask about financial aid, scholarships, or employer-sponsored reimbursement options.

5. Choose a Location That Works for You

Some programs are fully in-person. Others offer online or hybrid options. Choose the format that gives you the best shot at success.

Whether you’re balancing work and family or starting fresh, the right location and learning style make a big difference.

FlexTrades Can Help Pay for Training

Already working in the trades? FlexTrades offers a training reimbursement program for our technicians. You can receive up to $2,000 toward approved courses that build your trade knowledge and boost your career.

It’s one of the ways we invest in your future — because when you grow, we all win. 
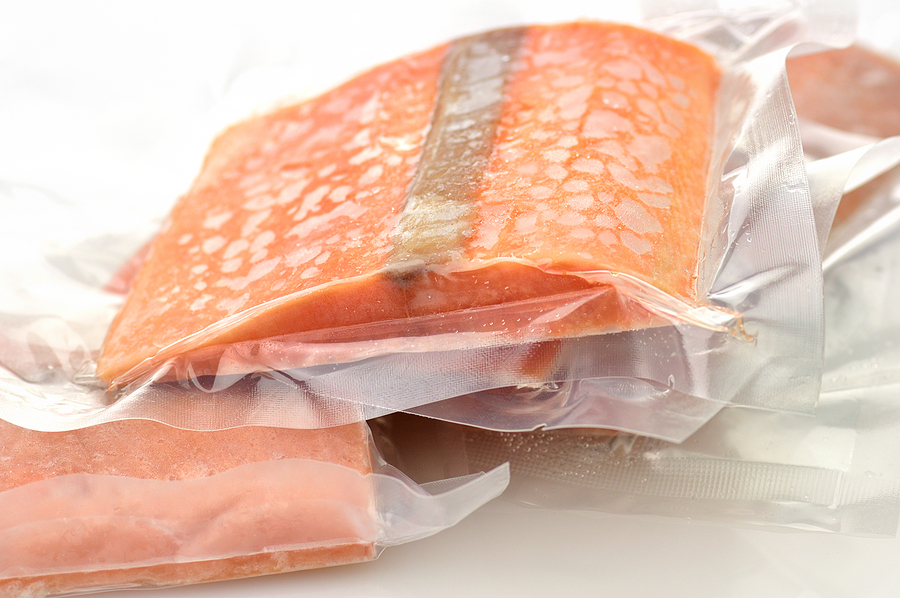
FlexTrades works with manufacturers of all kinds — from aerospace and automotive to food production. Some of our clients make frozen pizza. Others make snack cakes, breakfast foods, plant-based proteins, or prepared meals. The point is, we’re all pretty spoiled by the convenience of walking into a grocery store and grabbing whatever we want — frozen, fresh, or refrigerated.

But it wasn’t always like this.

Before the modern freezer, cold food storage meant digging holes in the ground, building underground cellars, or relying on blocks of lake ice stored in ice houses. The result? Slow freezing. That process formed large ice crystals, which caused food to become watery and tasteless once thawed.

Enter: Clarence Birdseye, the man who changed the game.

Clarence Birdseye: The Father of Frozen Foods

Clarence Birdseye got his start not in food, but in fur trading. While working in Canada, he noticed that fish caught by local Inuit froze instantly in the subzero air. Even months later, once thawed, the fish tasted just as fresh.

That moment of observation sparked a theory — fast freezing retains food’s texture and flavor better than slow freezing. Clarence tested his theory and proved it right, not once but twice.

Birdseye’s First Method: Calcium Chloride Brine

In his first innovation, Clarence developed a process using calcium chloride. Here’s how it worked:

  • Packaged food was placed between two metal belts
  • The belts were cooled to between -40°F and -45°F using a calcium chloride solution
  • The food froze almost instantly

This led to his first business — Birdseye Seafood — where he patented his process for freezing and storing fish.

His system included:

  • A refrigerating tank with calcium chloride brine
  • Containers to freeze fish fillets into solid blocks
  • Wax paper packaging for preservation
  • An insulated shipping container, later used in refrigerated railcars and grocery store display cases

Fun fact: Clarence also patented his refrigerated boxcar, laying the groundwork for modern cold-chain logistics.

From Bankruptcy to Breakthrough

Birdseye’s first venture went bankrupt. But he didn’t quit. He sold his and his wife’s life insurance policies and secured investment funding to launch again — this time with General Seafood Corporation in Gloucester, Massachusetts.

There, he developed a second freezing method, and this one stuck.

Birdseye’s Second Method: Ammonia and Innovation

This method used ammonia evaporation instead of calcium chloride. The process:

  • Packaged food was placed between hollow metal plates
  • Ammonia chilled the plates to between -25°F and -40°F
  • Fruits and vegetables froze to 0°F in 30 minutes, meats in 75 to 90 minutes

In 1929, Birdseye sold General Seafood Company — along with his fast-freezing patents — to Postum Cereal Company for $22 million (over $358 million today). Postum changed its name to General Foods Corporation and made Clarence president of its new Birds Eye Frosted Foods division.

Soon after, Birds Eye began rolling out frozen spinach, cherries, meats, and peas. That was just the beginning. Today, Birds Eye makes everything from frozen vegetables and sauced sides to full skillet meals and cauliflower wings.

An Inventor, a Naturalist, and a Relentless Innovator

Birdseye’s story began in Brooklyn in 1886. At age 10, he started his first business by trapping muskrats and selling them to a British lord. At Amherst College, he sold frogs to the Bronx Zoo to pay tuition. When that didn’t work out, he became a fur trader in Labrador and later worked as a naturalist for the U.S. government in the Arctic.

That’s where he got the idea that changed food manufacturing forever.

Through it all, Birdseye remained humble. His words say it best:

“I do not consider myself a remarkable person. I am just a guy with a very large bump of curiosity and a gambling instinct.”

Want to Learn More About Food Manufacturing?

Check out the FlexTrades blog for more How It’s Made stories — including articles on mystery flavored suckers, cheese, plant-based burgers, and even Spam

Every technician has a toolbox. Wrenches, pliers, screwdrivers — the mechanical staples are easy to recognize. But if you work in manufacturing, especially in quality or machining roles, there’s another set of tools that matter just as much: inspection tools.

These tools ensure the work you perform isn’t just done — it’s done right. And while some are provided by the employer (due to cost or required calibration), every technician should understand what these tools do and why they matter.

This is our version of the Essential Technician Toolbox, focused on quality operations.

Inspection Tools You Should Know

Calipers

Used to measure the inside diameter (ID) and outside diameter (OD) of components.

Types include:

Gauges

Used for quick, reliable dimensional checks.

  • Thread Gauges – also called screw or pitch gauges; measure thread pitch
  • Go/No Go Gauges – include plug, snap, and ring gauges for checking pass/fail limits (see the differences)
  • Chamfer Gauges – measure top diameters of tapered or chamfered holes
  • Depth Gauges / Depth Micrometers – measure holes, slots, and cavities
  • Height Gauges – measure and set vertical distances

Hardness Testers

Used to determine the Rockwell Hardness of materials. The method depends on the type of metal or alloy being tested.

Indicators

Help align parts, inspect roundness, or assess surface irregularities.

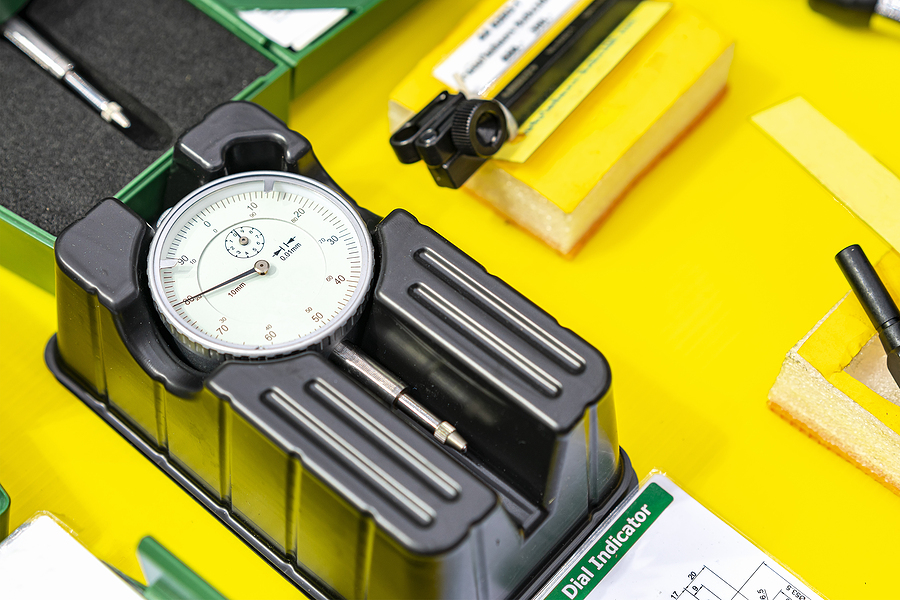
  • Dial Test Indicators
  • Plunge Indicators
  • Travel Indicators

Micrometers

Precision instruments that measure thickness, depth, and length — more exact than calipers.

Surface Comparators

Used to visually compare and measure surface roughness or finish.

Surface Plates

Granite or cast iron blocks that provide a perfectly flat reference surface for checking whether an object is flat, convex, or concave.

Tool Tidbits: Analog vs. Digital and Metric vs. Imperial

Many of the tools listed above come in both analog and digital formats. Think of it like this:

  • Analog tools = like a watch with hands
  • Digital tools = like a digital clock, giving precise numbers at a glance

Similarly, these tools may use metric or imperial systems. Not sure what that means? Check out this guide.

Calibration Matters

Accuracy is everything. That’s why inspection tools must be regularly calibrated. Calibration ensures that your readings are reliable, consistent, and within tolerance — because trust in the tool means trust in the work.

Who Uses These Tools?

If you’re in any of the following roles, these tools are part of your world:

  • CNC Operators
  • CNC Machinists
  • Quality Inspectors
  • CMM Programmers
  • Machine Operators

These professionals rely on inspection tools during pre-inspection, in-process checks, and final inspection to make sure every part meets spec.

Because in manufacturing, it’s always safety first, quality second — and these tools help protect both. 

In manufacturing, people often think that production volume is the top priority. That’s a mistake.

At FlexTrades, we know the truth: safety always comes first. And right behind that is quality — because without quality, production numbers don’t matter.

Critical to achieving consistent, measurable quality is a powerful piece of equipment: the CMM.

Let’s take a closer look at what CMMs are, how they work, and why they matter.

What Is a CMM?

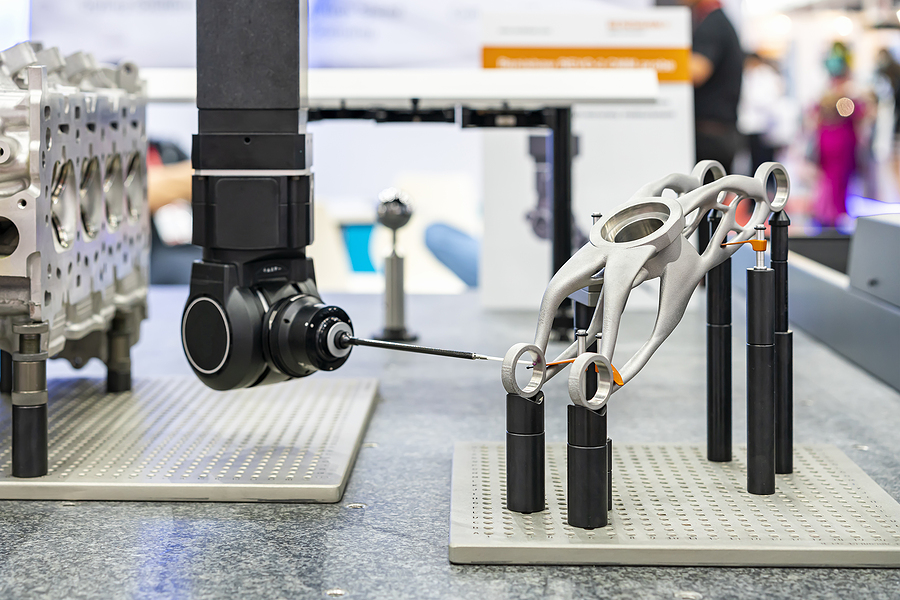
CMM stands for Coordinate Measuring Machine. These machines are used to measure the physical dimensions and geometric characteristics of manufactured parts.

Yes, those same measurements can be done with precision hand tools. But manual inspection leaves room for error. People get tired. Vision blurs. Mistakes happen.

CMMs eliminate that guesswork by automating the inspection process. At a basic level, a CMM includes:

  • A stable platform or table to position the part
  • A probe that performs the measurements
  • A computer program that guides and controls the probe’s path

But as simple as that sounds, there’s more going on under the hood.

CMM Programming: Where Precision Begins

CMMs are only as smart as the code that runs them.

CMM programming is a specialized form of machine instruction. Programmers create sequential sets of directions that tell the probe where to move, what to measure, and how to measure it.

Some parts only require a few basic measurements. Others have hundreds of features that must meet tight tolerances. Regardless of complexity, the program must be flawless — because CMMs can’t measure anything they haven’t been told to inspect.

CMM programming is done using software specifically designed for this task. If you’re not a programmer, it might look like a foreign language. But to a trained CMM programmer, it’s a tool for perfection.

What Does a CMM Programmer Do?

A CMM Programmer writes the detailed code required to inspect parts accurately and efficiently.

That includes:

  • Mapping the inspection path
  • Defining each feature and tolerance
  • Ensuring alignment between design specifications and machine behavior

As machined parts become more complex — with intricate geometries and tighter tolerances — the job only gets harder. CMM programmers play a key role in maintaining quality and reducing waste across the entire production cycle.

Interested in Becoming a CMM Programmer?

If you’re looking to break into this field, start by exploring programs in Quality and Manufacturing Technologies. Many trade schools and technical colleges offer degrees or certificates in these areas.

Once you’ve got the education, hands-on experience is next. Common starting points include:

  • CMM Operator
  • Quality Inspector
  • Machine Operator with inspection responsibilities

If you’re already in manufacturing, let your interest be known. Many CMM programmers start out on the floor and transition into programming roles through on-the-job training.

Already a CMM Programmer or Operator?

FlexTrades is hiring skilled professionals like you. Join our team and get access to:

  • National travel opportunities
  • Advanced technology and equipment
  • Flexible schedules
  • Industry-leading manufacturers

Apply here and take the next step in your career. 

At FlexTrades, we provide workforce solutions to American manufacturers. It’s what we do — and we take the solution part seriously.

That means we ask a lot of questions. But we also answer a lot, especially from the skilled trades community. This post tackles some of the most frequently asked questions we hear from technicians and job seekers alike.

Do I Need a Forklift Certification?

This is one of the most common questions we get. And the answer is straightforward:

No, you don’t need an active forklift certification to qualify for a FlexTrades project.

But — and it’s a meaningful but — having prior forklift experience or past certification is highly preferred.

Here’s why: any technician operating a forklift on a project will need to certify to that client’s internal standards while onsite. So while FlexTrades doesn’t require your certification to be current, previous certification makes you a stronger candidate and helps you hit the ground running.

Are There Other Required Certifications?

Yes, there are a few other certifications that occasionally come into play:

  • OSHA safety certifications (Occupational Safety and Health Administration)
  • MSHA safety certifications (Mine Safety and Health Administration)
  • CDLs (Commercial Driver’s Licenses) for roles involving transportation or heavy hauling

These certifications aren’t required for every project, but when they are, having them in hand puts you at the top of the list.

What Other Certifications Should I Consider?

Beyond the essentials, there are plenty of optional certifications that can make you more competitive in the skilled trades.

Want to get ahead? These resources can help:

Certifications can lead to better roles, higher wages, and more career mobility.

Want to Work with FlexTrades?

If you’re a recent graduate of a technical training program, consider applying through the FlexTrades ReTool Program. It’s designed to help you bridge the gap between training and the real world.

Already have experience? Join our Talent Network to access new projects, grow your career, and work with top-tier U.S. manufacturers.

Have a Question of Your Own?

We want to hear it. Send your questions to writingteam@flextrades.com and we’ll answer them in a future FAQ. 

The art of metal casting — melting metal, pouring it into molds, and shaping it into usable forms — is as old as civilization itself. Archeologists have uncovered metal casting relics from as early as 300 BC, possibly even older, depending on who you ask.

Most of the oldest artifacts come from Mesopotamia, where early craftspeople used clay molds and fire pits to cast copper, gold, and silver. It was here that the first alloy — bronze, a mix of copper and tin — was born. That single innovation sparked a new era of metal tools, weapons, and technology.

But like every great invention, metal casting has evolved. And the reasons are as much about human progress as they are about science.

Why Metal Casting Changed Over Time

Two major shifts drove the evolution of foundries:

  • Humans stopped migrating and started settling, giving rise to cities, economies, and steady production
  • Mining technology improved, giving us access to more raw material in less time

The result? Foundries got bigger, smarter, and more influential — shaping everything from warfare to water systems.

Foundry Highlights from the 19th Century

By the 1800s, metal casting was more than craft. It was an industry. The 19th century brought several major advancements:

  • Open-hearth furnaces for higher-quality steel
  • Sandblasting to clean castings faster and more effectively
  • Gear-tilted ladles to pour molten metal more safely

This era helped drive the industrialization of the United States, with foundries fueling the construction of railroad tracks, ironclad warships, and even America’s first submarine, launched in 1881.

Breakthroughs in the 20th Century

The 1900s ushered in a wave of innovation:

  • The coreless electric induction furnace changed how we melt metal
  • Low-carbon stainless steel opened up new use cases
  • Foundries began serving defense, aerospace, HVAC, and automotive sectors

This century saw foundries expand rapidly across North America. They became central to U.S. manufacturing.

Fun Fact:
The American Foundry Society (AFS) first met in 1896, but its first student chapter wasn’t launched until 1907 — in Minnesota. That same year, a patent was issued for high-pressure die casting machinery, a technology still used today.

The Foundry Industry Today

Metal casting remains a cornerstone of manufacturing — just more advanced than ever.

Today, the U.S. foundry industry is worth over $33 billion, with close to 1,900 active foundries and nearly 200,000 workers. Metal castings are found in 90% of durable goods, from clean water systems and farm equipment to energy infrastructure and transportation components.

And the modern foundry? It’s high-tech.

Many now use:

  • CAD software for design
  • 3D printing for mold creation
  • Robotics and automation for efficiency
  • Casting analysis to improve quality and reduce waste

Foundries have never been more precise — or more important.

See It for Yourself

Want a closer look? Revisit our article on how steel is made and check out this factory tour of the St. Paul Foundry. You’ll see molten metal in action and the incredible technology that brings modern castings to life.

After that, look around. From the water pipes beneath your feet to the machine parts running your factory — metal castings are everywhere

The National Institute for Occupational Safety & Health (NIOSH) defines Personal Protective Equipment (PPE) as the last line of defense in preventing workplace injuries, illnesses, and fatalities.

That means PPE doesn’t replace smart design or safer processes — but when a hazard slips through the cracks, PPE protects the individual. It can be the difference between a close call and a serious injury.

Here at FlexTrades, we believe safety starts with knowledge. So we’ve put together a quick breakdown of essential PPE and how to use it.

The Four Basic Categories of PPE

While each job site is different, PPE typically falls into one of four categories:

  • Face and Eye Protection
  • Respiratory Protection
  • Skin and Body Protection
  • Hearing Protection

A hazard assessment will help you determine which equipment is necessary. Below, we break down each category and offer practical tips to help you get it right.

Face and Eye Protection

This type of PPE shields you from sprays, splashes, flying objects, and high-heat tasks like welding.

Common examples include:

  • Goggles
  • Safety glasses
  • Face shields
  • Welding visors

Pro Tip: Always make sure your eyewear meets ANSI Z87.1 standards. Inspect lenses regularly for cracks or wear.

Respiratory Protection

Respiratory PPE is essential when you’re exposed to dust, fumes, gases, or biological hazards. It protects your lungs, airways, and internal organs.

Examples include:

  • Full-face respirators
  • Self-contained breathing apparatus (SCBA)
  • Gas masks
  • N95 masks and surgical masks

Pro Tip: Always fit test respirators and replace filters regularly to maintain effectiveness.

Skin and Body Protection

This category is broad — it includes anything designed to protect your skin or body from burns, cuts, impact, chemical exposure, or falls.

Key areas of protection:

  • Head – Hard hats, bump caps
  • Body – Safety vests, flame-resistant suits
  • Hands – Cut-resistant gloves, heat shields
  • Feet – Steel-toe boots, anti-slip soles
  • Fall – Harnesses, lanyards, and anchor points

Pro Tip: If gear is damaged or contaminated, replace it immediately. Compromised PPE isn’t PPE at all.

Hearing Protection

Loud environments can lead to long-term hearing damage if proper protection isn’t used.

Options include:

  • Earmuffs
  • Earplugs
  • Ear caps

Pro Tip: Hearing protection is only effective if it fits properly. Dirty or worn equipment should always be discarded.

Your PPE Checklist Starts Here

If you’re not sure where to begin, use this guide as a PPE checklist to support your next hazard assessment. Improving your understanding of safety gear is a simple but powerful way to strengthen your facility’s safety culture.

Want to go further? Revisit our Every Technician’s Toolbox blog to learn more about PPE and other essential safety practices.

And if you already know your way around all this gear, you might be ready for your next opportunity in manufacturing. Send your resume to retoolrecruiting@flextrades.com and let’s see where you belong. 

At FlexTrades, we believe in supporting American manufacturing from every angle — not just by providing workforce solutions, but by advocating for the skilled trades and the technical education that fuels them.

That’s why we’re kicking off this year’s Monthly Manufacturing Calendar Highlight with a reminder: CTE Month® begins February 1st.

This is your chance to celebrate, support, and elevate the future of the skilled trades. Let’s talk about what CTE Month is and how you can get involved.

What Is CTE Month?

Career and Technical Education (CTE) helps students of all ages prepare for high-wage, high-demand careers. And we’re not just talking about students in high school — adult learners, returning workers, and veterans are part of the movement, too.

CTE Month happens every February as a nationwide campaign to:

  • Raise awareness about CTE’s role in workforce development
  • Celebrate CTE programs and their achievements
  • Encourage partnerships between educators, employers, and policymakers

You may have even seen it featured during events like the Super Bowl — like this commercial from Oklahoma Career Tech.

How Can You Celebrate CTE Month?

Whether you’re an educator, employer, or just someone who believes in the power of skilled trades, there are plenty of ways to get involved:

  • Instructors / Educators: Host a tour or open house. Let the community see what CTE looks like up close.
  • Businesses / Employers: Partner with local schools or host a job fair. Share success stories about CTE graduates on your team.
  • Graduates / Technicians: Speak up. Share your story publicly. The Skills Gap grows wider when people don’t understand the value of your experience.
  • Everyone Else: Download a CTE Month Zoom background and use it during virtual meetings to show your support — no speech required.
  • No matter your role, there’s a way to advocate for CTE this month. Sometimes, all it takes is showing up and being visible.

What’s Next?

February is just the start. Manufacturing advocacy doesn’t stop with CTE Month. In fact, October and MFG Day will be here before you know it.

So get involved. Be loud. Share your story. Support the people and programs building the future of American manufacturing.

And if you know of an industry event worth highlighting, email our Writing Team — we’d love to feature it in the months ahead. 

Manufacturing sits at the intersection of science, technology, engineering, and math. It’s where ideas become tangible and precision meets production. But behind the machinery and the measurements is a set of principles that most of us first encountered in a middle school science class.

So today, let’s talk about something that sounds simple but plays a massive role in manufacturing: static electricity.

What Is an Atom, and Why Does It Matter?

To understand static electricity, we have to go all the way down to the atomic level.

Everything you can touch, build, or break is made of atoms. These atoms are made up of particles — protons, electrons, and neutrons — centered around a nucleus. Here’s the shorthand:

  • Protons have a positive charge
  • Electrons have a negative charge
  • Neutrons are, as the name suggests, neutral

In most materials, the number of protons and electrons is equal, so the object carries no electrical charge. But rub two materials together — especially ones with different conductive properties — and you disrupt that balance. Electrons jump from one surface to another, leaving one object more negative and the other more positive.

That imbalance? That’s static electricity.

Want to dig deeper into atomic structure? Start here.

Conductors vs. Insulators

Not all materials behave the same. Some let electrons move freely. Others don’t.

  • Conductors (like water and metal) have loosely bound electrons, making them ideal for electron transfer
  • Insulators (like rubber and plastic) hold electrons tightly, limiting their movement

This difference is critical in understanding how static electricity forms — and how it affects real-world environments.

The Balloon & Hair Trick

It’s a classic. You rub a balloon on your head and your hair starts to rise. But why?

Rubber is an insulator, so it doesn’t let electrons move easily across its surface. Hair, on the other hand, acts more like a conductor. When you rub the balloon on your head, electrons from your hair transfer to the balloon. The balloon now has more electrons (and becomes negatively charged), while your hair has fewer electrons (becoming relatively positive).

That difference in charge is static electricity. And it’s strong enough to pull your hair toward the balloon.

Fun? Sure. But in a manufacturing setting, it’s a different story.

Static Electricity in Manufacturing

Static electricity can be dangerous in a production environment. It’s not just an annoying zap. It’s a legitimate safety and quality risk.

Electrostatic discharge (ESD) — that tiny shock you sometimes feel when touching a doorknob — can do real damage. In manufacturing, ESD can:

  • Ignite flammable gases or vapors
  • Destroy sensitive electronic components
  • Attract dust and particles in cleanrooms
  • Cause materials to stick together or misalign

That’s why manufacturers go to great lengths to manage it.

How Manufacturers Manage Static Electricity

To minimize the risks of ESD, many facilities use specialized tools and processes, including:

  • ESD-safe clothing to reduce charge buildup
  • Antistatic wrist straps and grounding bracelets to safely redirect charges
  • ESD mats to neutralize static underfoot
  • Zero-charge hand lotions and cleaners to reduce friction on skin
  • Controlled humidity to reduce airborne electron movement

In highly controlled environments — especially in electronics manufacturing — these precautions aren’t optional. They’re essential.

Want to Learn More?

FlexTrades has a growing library of How It’s Made content that explores the science behind the trades. Check out more on our blog and see what else goes into the work behind the work.

What’s the craziest thing you’ve ever done? What about the most charitable?

At FlexTrades, we like to answer both questions with one story — the Polar Plunge.

If you’re not familiar, the Polar Plunge is a national fundraising event where brave souls jump into icy water in support of Special Olympics. It’s cold. It’s intense. And it’s one of the most rewarding things we do all year.

In Minnesota alone — where, by the way, we have 14,000+ lakes, not just the 10,000 you’ve heard about — this event is a big deal. Every winter, people cut holes in thick sheets of lake ice and dive in. For a cause. For the community. And for the joy of doing something that matters.

About the Special Olympics

The Special Olympics started small. In 1962, Eunice Kennedy Shriver hosted the first “Camp Shriver” in the backyard of her Maryland home. She wanted kids with intellectual disabilities to have a place to play, grow, and belong — because, at that time, they were often excluded from mainstream programs.

That first camp became an annual tradition, then a movement. On July 20, 1968, more than a thousand athletes from the U.S. and Canada came together in Chicago for the first International Special Olympics Summer Games.

Today, that same movement spans over 170 countries and reaches more than 5 million athletes worldwide. And it all started with one idea: everyone deserves a chance to compete.

My Personal Why

My support for Special Olympics didn’t begin with a plunge. It began with my cousin, Joey.

Joey was born with Down syndrome in 1960, during a time when children with special needs were often institutionalized and separated from their families. His parents were part of a generation that pushed back — advocating for inclusion before it had a name. And they found community and opportunity through Special Olympics.

By the time I was born, Joey was already competing regularly. Over his lifetime, he took part in more than two dozen Minnesota state games and a handful of national events. The skills, pride, and friendships he gained from competition changed his life — and the lives of those around him.

When I started my career at FlexTrades in 2017, I knew I wanted to support that mission more actively. That’s when I joined my first Polar Plunge.

FlexTrades Supports the Special Olympics

The experience was everything I’d hoped for and more — fun, moving, energizing. I couldn’t stop talking about it. And by the following year, several coworkers joined me.

That was the start of our official FlexTrades Plunge Team.

Since then, we’ve raised more than $14,000 for Special Olympics Minnesota. To put that in perspective: just $500 is enough to launch a new delegation in the state. It’s proof that a little support can go a long way.

Support Our 2022 Polar Plunge

Our fifth plunge took place on February 19, 2022, in Prior Lake, Minnesota. Even if you weren’t in the state — or willing to jump in yourself — there were still plenty of ways to get involved.

  • Plunge virtually — or toss something silly into the lake in your place (rubber chicken, anyone?)
  • Donatesupport the FlexTrades team directly
  • Show up — spectators are always welcome and encouraged
  • Share your support — a few kind words on social media go a long way

And if you’re feeling inspired, you can start a plunge of your own no matter where you live.

Let’s Keep It Going

If you have questions about Special Olympics, the Polar Plunge, or how FlexTrades supports the cause, reach out to us at writingteam@flextrades.com.

And remember the athlete’s oath that has guided Special Olympics for decades:

“Let me win. But if I cannot win, let me be brave in the attempt.”